Future Trends in Ball Valve Manufacturing: The All-in-One Machine Advantage
Release time:
Oct 07,2025
Future Trends in Ball Valve Manufacturing: The All-in-One Machine Advantage Table of Contents 1. Introduction to Ball Valve Manufacturing 2. Understanding Ball Valves - 2.1 Types of Ball Valves - 2.2 Importance of Ball Valves in Various Industries 3. Current Challenges in Ball Valve Manufacturing 4. The All-in-One Machine Technology - 4.1 Features and Benefits of All-in-One

Future Trends in Ball Valve Manufacturing: The All-in-One Machine Advantage
Table of Contents
1. Introduction to Ball Valve Manufacturing
2. Understanding Ball Valves
- 2.1 Types of Ball Valves
- 2.2 Importance of Ball Valves in Various Industries
3. Current Challenges in Ball Valve Manufacturing
4. The All-in-One Machine Technology
- 4.1 Features and Benefits of All-in-One Machines
- 4.2 Case Studies: Success with All-in-One Machines
5. Future Trends in Ball Valve Manufacturing
- 5.1 Automation and Industry 4.0
- 5.2 Sustainability in Manufacturing Practices
6. Impact on Productivity and Costs
7. Conclusion
8. FAQs
Introduction to Ball Valve Manufacturing
In the realm of industrial equipment, ball valves are essential components used to control the flow of liquids and gases. As we look to the future, innovations in manufacturing processes are set to reshape the ball valve industry. The emergence of **All-in-One machine technology** promises to enhance production capabilities while addressing current challenges faced by manufacturers.
Understanding Ball Valves
Ball valves are widely used due to their ability to provide a reliable seal, making them ideal for high-pressure applications. Their design allows for quick opening and closing, which is crucial in various industrial processes.
Types of Ball Valves
Several types of ball valves exist, including:
- **Full Port Ball Valves**: These allow for unrestricted flow, ideal for applications requiring maximum throughput.
- **Reduced Port Ball Valves**: These have a smaller opening, resulting in lower flow capacity but are cost-effective for many applications.
- **Trunnion Mounted Ball Valves**: These are designed for high-pressure environments, providing stability and improved sealing.
Importance of Ball Valves in Various Industries
Ball valves find applications in various sectors, including:
- **Oil and Gas**: For controlling flow rates in pipelines.
- **Water Treatment**: In controlling the flow of water and chemicals.
- **Chemical Processing**: For handling corrosive substances safely.
Current Challenges in Ball Valve Manufacturing
Manufacturers face several challenges, including:
- **Quality Control**: Ensuring that all valves meet stringent industry standards.
- **Production Efficiency**: Balancing speed with quality to meet increasing demand.
- **Cost Management**: Reducing manufacturing costs while maintaining high standards.
The All-in-One Machine Technology
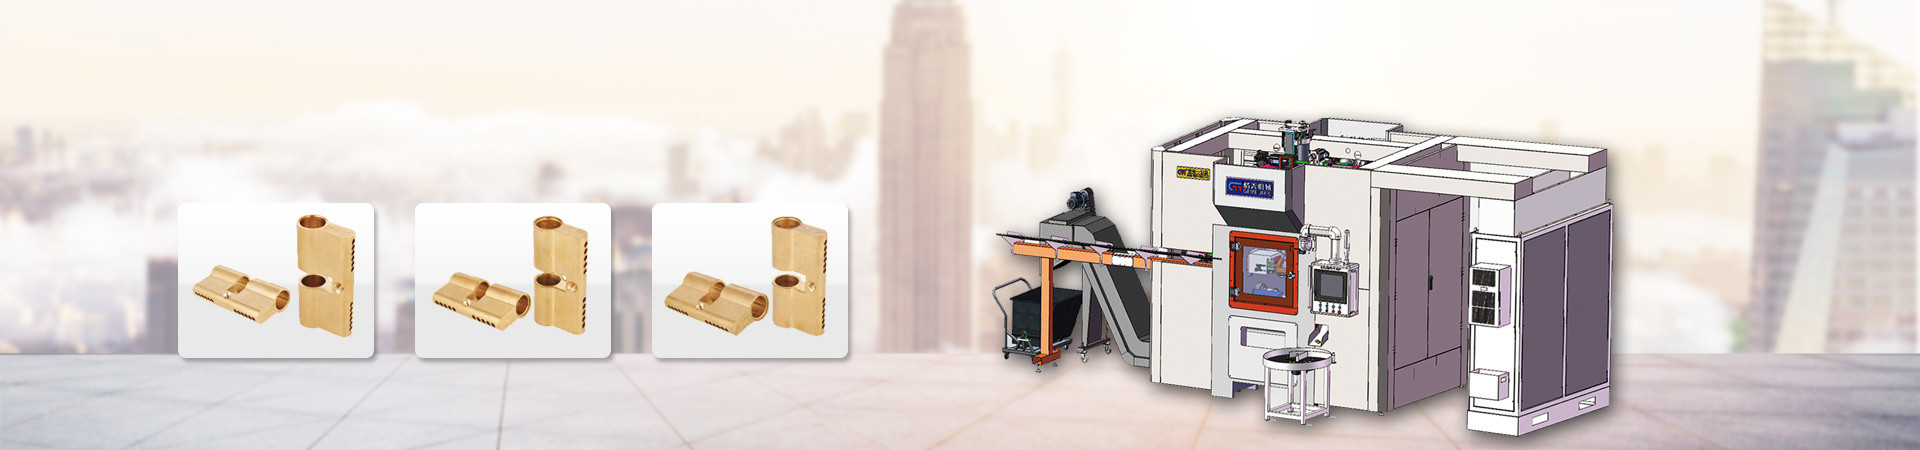
The All-in-One machine represents a significant technological advancement in valve manufacturing. This integrated system combines multiple machining processes into a single unit, providing a streamlined production line.
Features and Benefits of All-in-One Machines
- **Automation**: Incorporates automated processes that reduce manual intervention, leading to fewer errors.
- **Space Efficiency**: Reduces the need for multiple machines, optimizing floor space.
- **Cost-Effectiveness**: Lowers operational costs due to decreased energy consumption and maintenance needs.
- **Increased Productivity**: Enables faster production cycles without compromising quality.
Case Studies: Success with All-in-One Machines
Several companies have adopted All-in-One machines with remarkable success. For instance, a leading valve manufacturer reported a **30% increase in production** efficiency within the first year of implementation. Another company highlighted a **20% reduction in manufacturing costs**, showcasing the technology's economic advantages.
Future Trends in Ball Valve Manufacturing
As the industry continues to evolve, several trends are emerging that will shape the future of ball valve manufacturing.
Automation and Industry 4.0
The integration of smart technologies in manufacturing processes is a key trend. **Industry 4.0** introduces the use of IoT, AI, and machine learning to optimize production and maintenance. This connectivity allows manufacturers to monitor real-time data, facilitating predictive maintenance and reducing downtime.
Sustainability in Manufacturing Practices
Sustainable manufacturing is becoming increasingly important. Companies are adopting eco-friendly practices, such as using recyclable materials and reducing waste. Implementing energy-efficient machines contributes to lower carbon footprints and aligns with global sustainability goals.
Impact on Productivity and Costs
The adoption of All-in-One machines and other innovative manufacturing technologies significantly impacts productivity and costs. Enhanced automation leads to faster production times, while reduced operational costs improve profit margins. Moreover, ensuring consistent quality minimizes the risk of defects and customer returns, further enhancing the bottom line.
Conclusion
The future of ball valve manufacturing is bright, driven by technological advancements such as the All-in-One machine advantage. These innovations not only address current manufacturing challenges but also pave the way for increased efficiency, sustainability, and profitability in the industry. As manufacturers embrace these changes, they will position themselves for success in an ever-evolving market.
FAQs
**1. What are the main advantages of All-in-One machines in ball valve manufacturing?**
All-in-One machines streamline production processes, enhance automation, reduce operational costs, and increase overall efficiency.
**2. How do ball valves differ from other types of valves?**
Ball valves provide a reliable seal and quick flow control, making them superior for high-pressure applications compared to other valve types.
**3. What are the key industries utilizing ball valves?**
Ball valves are primarily used in oil and gas, water treatment, and chemical processing industries due to their reliability and efficiency.
**4. How is automation impacting the ball valve manufacturing industry?**
Automation increases production efficiency and consistency, reduces labor costs, and allows for real-time monitoring of manufacturing processes.
**5. What role does sustainability play in modern ball valve manufacturing?**
Sustainability is essential as manufacturers adopt eco-friendly practices, reduce waste, and implement energy-efficient technologies to align with global standards.
Related News
From Concept to Reality: Building an All-in-One Machine for Fire Sprinkler Heads
From Concept to Reality: Building an All-in-One Machine for Fire Sprinkler Heads Table of Contents 1. Introduction to Fire Sprinkler Systems 2. The Importance of Fire Sprinkler Heads in Safety 3. Conceptualizing the All-in-One Machine 4. The Design Process: From Idea to Blueprint 5. Addressing Engineering Challenges 6. Manufacturing the All-in-One Machine 7. Testing and Quality Assu
The Essential Role of Floating Ball Valve All-in-One Machines in Modern Hardware
The Essential Role of Floating Ball Valve All-in-One Machines in Modern Hardware Hardware tools play a crucial role in various industries, from construction to manufacturing. Among these indispensable tools, **floating ball valve all-in-one machines** have emerged as vital components, enhancing efficiency and functionality in modern hardware applications. This article delves into the significance
Enhancing Supply Chain Efficiency: The Comprehensive Benefits of All-in-One Ball Valve Solutions
Enhancing Supply Chain Efficiency: The Comprehensive Benefits of All-in-One Ball Valve Solutions Table of Contents 1. Introduction to Supply Chain Efficiency and Ball Valves 2. What Are All-in-One Ball Valves? 3. The Importance of Supply Chain Efficiency in Industrial Operations 4. Benefits of All-in-One Ball Valve Solutions 5. Applications of Ball Valves Across Industries
Contact Us
Address: No.5, Meiyuxi 1st Road, Yuanmei Village, Luncang Town, Nanan City, Quanzhou City, Fujian Province
Contact: Zeng Manager
Mobile phone: +8615985886969 / +8617689338707/ +8617607975000
E-mail:1656573095@qq.com
Website:http://www.gemeimachinery.com
Youtube website:https://www.youtube.com/@user-tw5mf7ms7w
Add WeChat
Add WeChat
Copyright©2024 Quanzhou Gemei Machinery Equipment Co.,LTD | Business License | Powered by:www.300.cn | SEO Tags